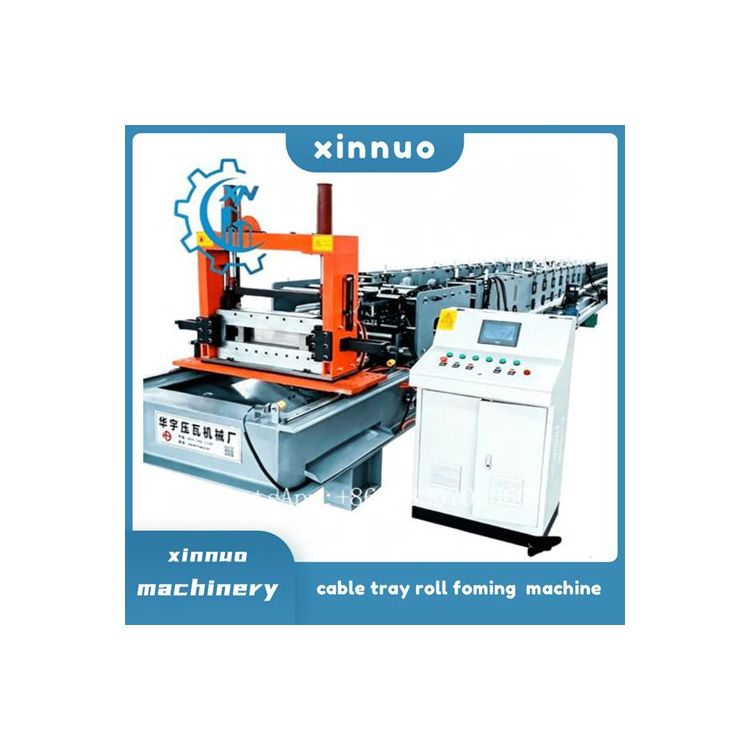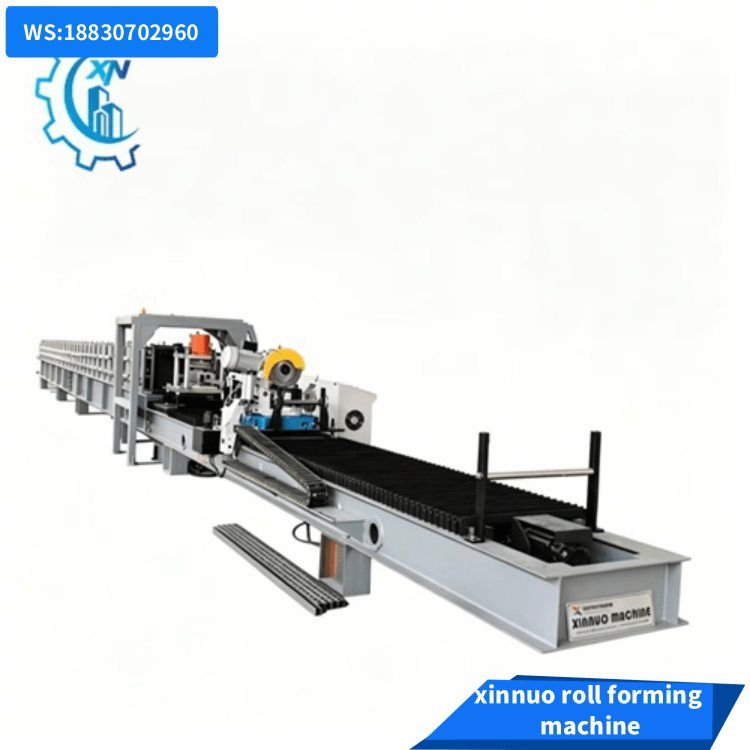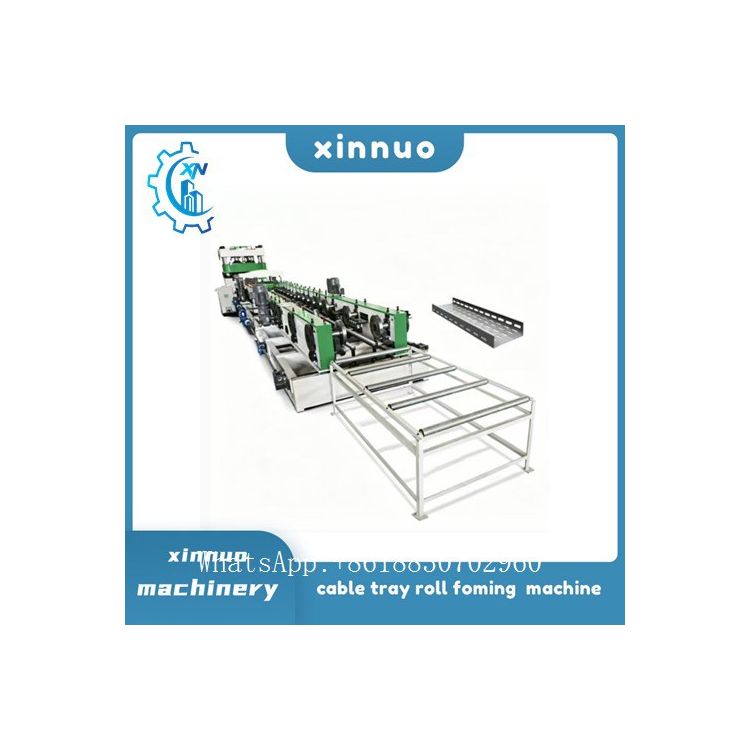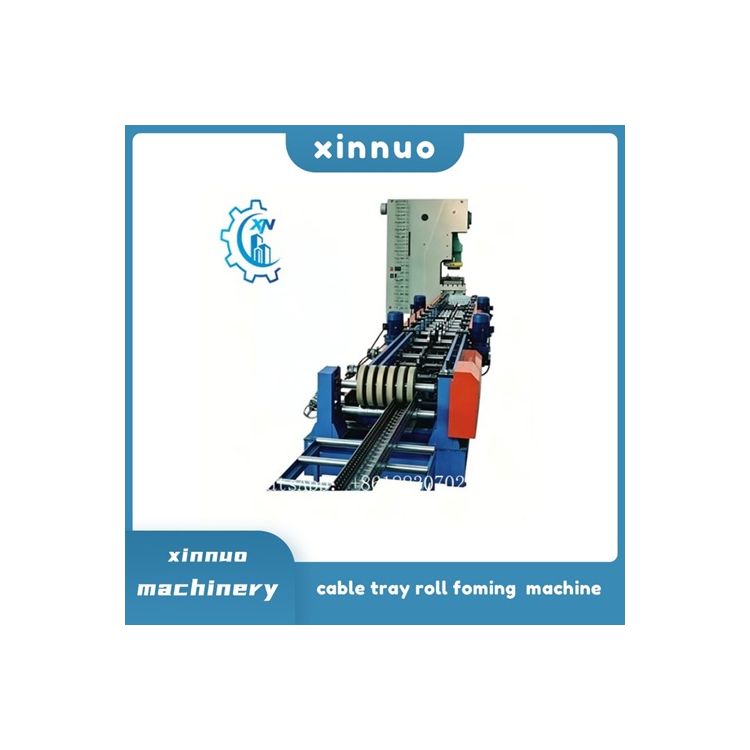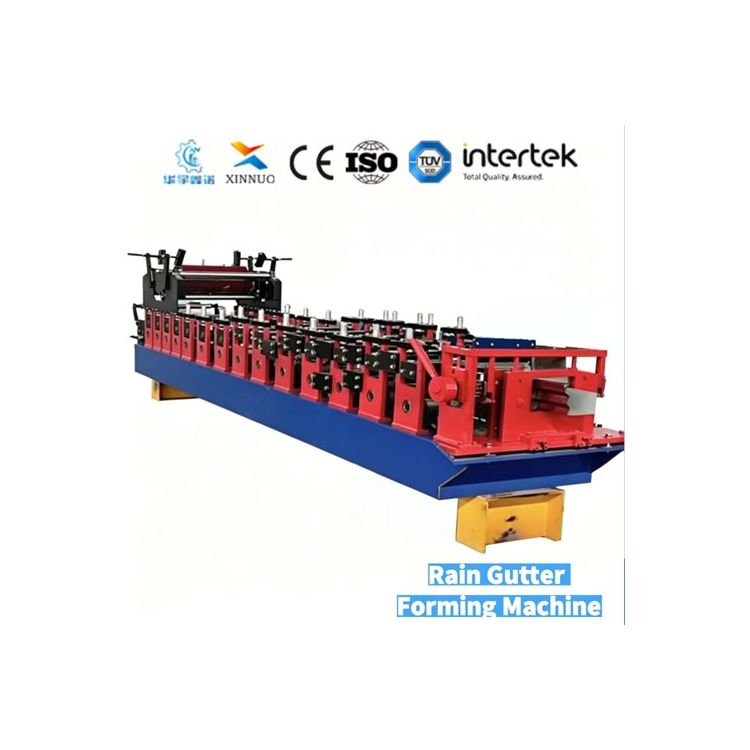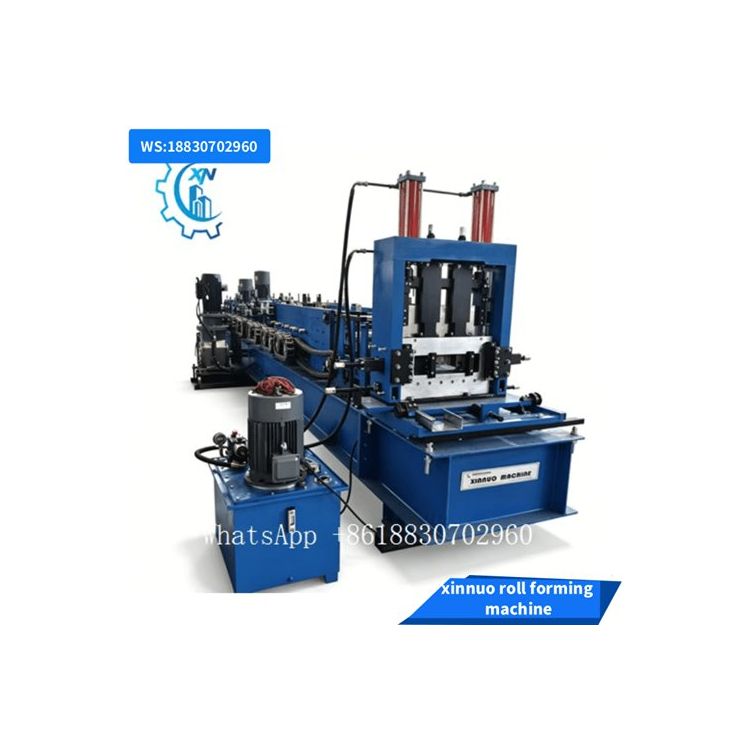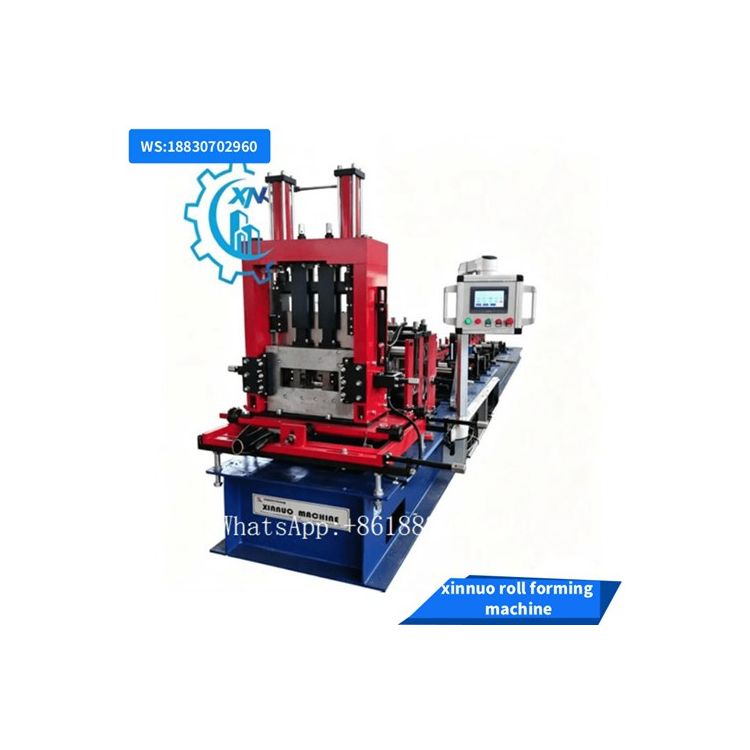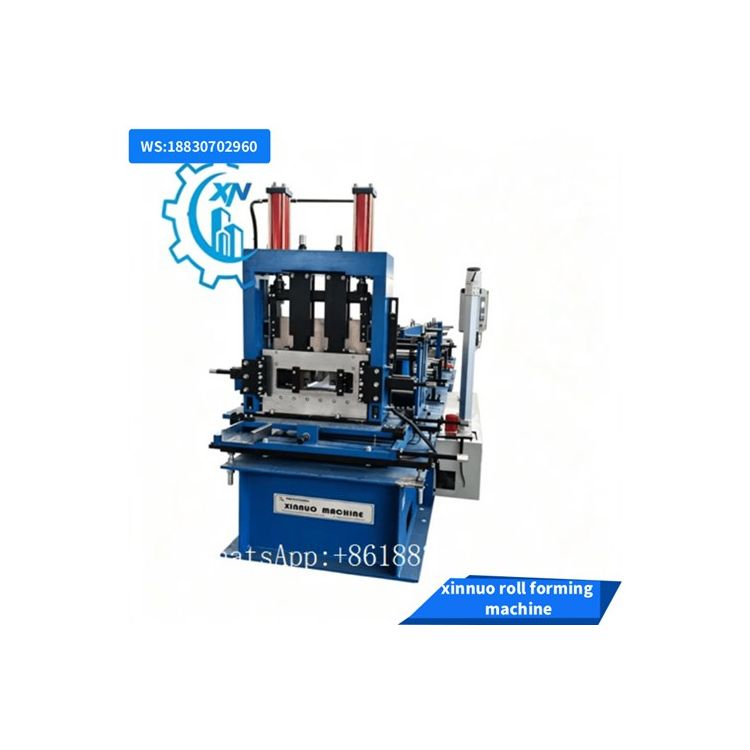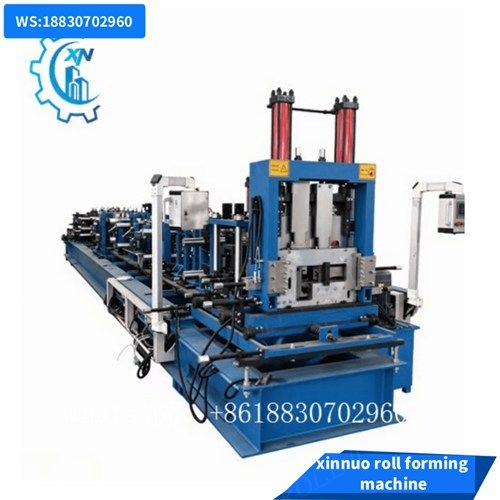
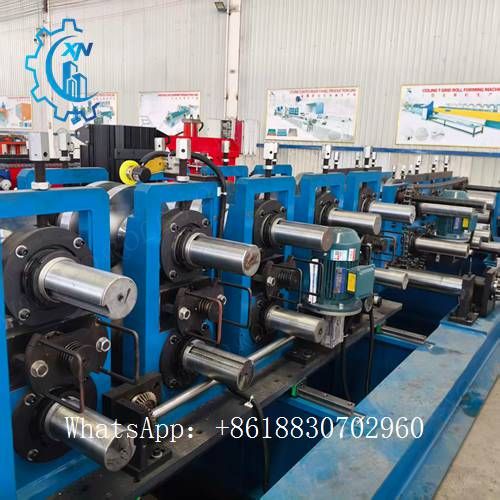
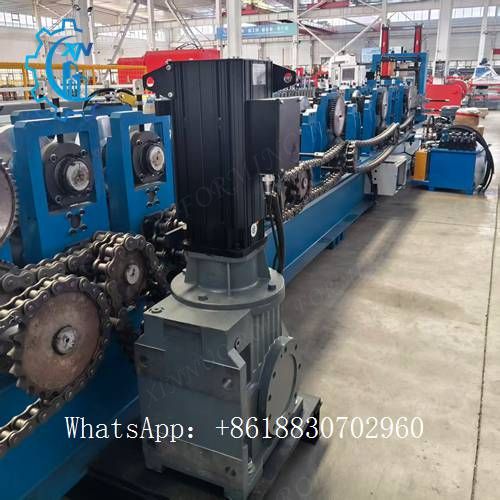
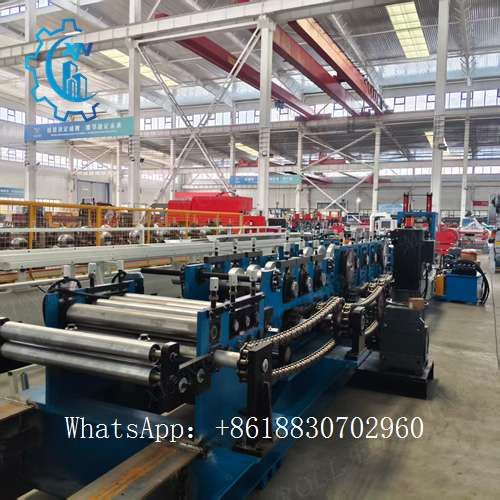
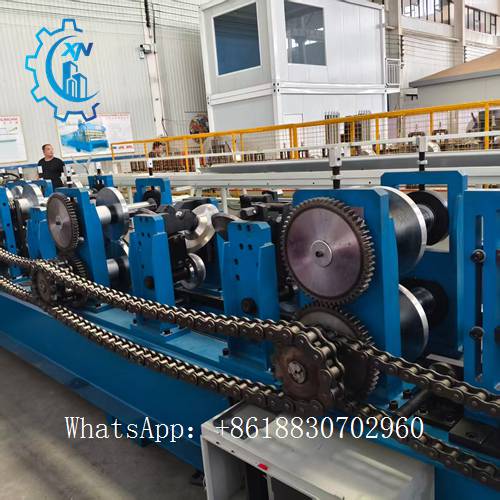
XN300 CZ purlin roll forming machine,accordingly a classic model designed for mid to high-end customers seeking exceptional performance and stability.
With 21 roll forming stations, this machine offers double straightening for higher accuracy, ensuring your output meets the highest standards.
The width range of 80-300mm and thickness range of 1.0-3.0mm provides versatility in production and can meet the needs of various projects.
Define the smallest and largest C and Z sections before selecting the line. Material thickness must be reviewed together with grade, yield strength and geometry. For the adjustment sequence, see C/Z changeover and setup.
A combined line is useful when a workshop needs both C and Z sections. Confirm the supported section family and whether switching requires manual adjustment, motorized movement or a tooling change.
Compare the total setup process, including punching, cutoff and first-piece checks, against your batch sizes.
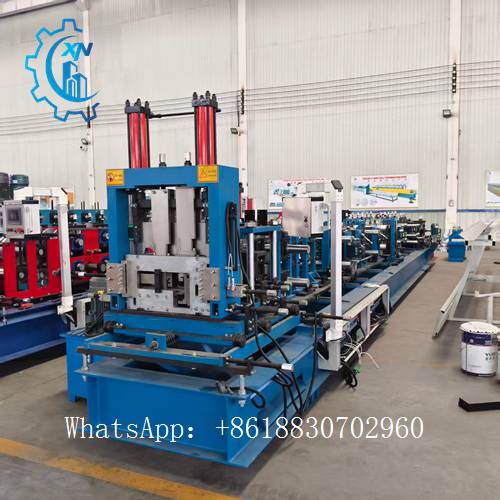
The order of punching and cutting depends on the approved line layout. Review complete purlin line configuration for module selection.
| Decoiler | Coil weight, width, inside diameter and loading method |
|---|---|
| Feeding | Strip guidance, loop arrangement and line control |
| Leveling | Incoming coil condition and material range |
|---|---|
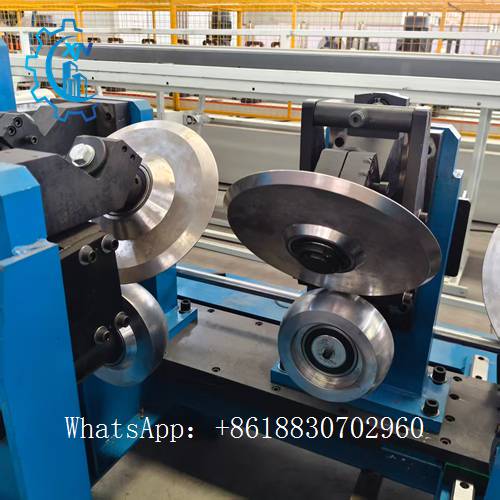
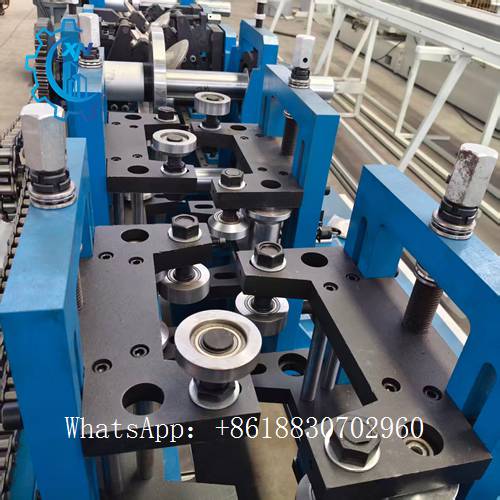
| Roll tooling | C and Z drawings, bend radii and coating requirements |
| Drive and adjustment | Drive arrangement, size adjustment and C/Z switching steps |
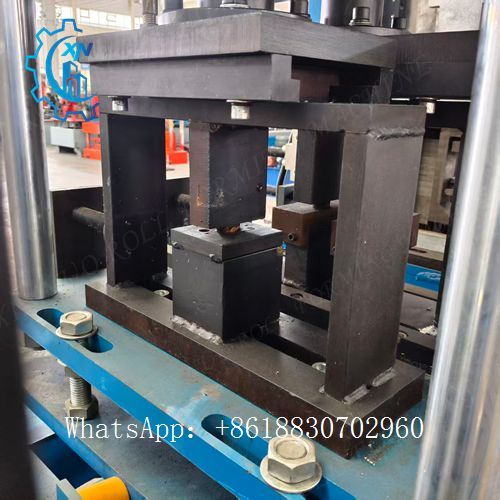
| Punch location | Web and flange holes required by the drawing |
|---|---|
| Hole tooling | Round holes, slots, sizes, pitch and tool changes |
| Cutoff tooling | Supported profile sizes, section orientation and cut-end quality |
| Cutoff sequence | Stop-to-cut or flying-cut arrangement for the output target |
| Part size | Minimum/maximum length and section weight |
|---|---|
| Stacking arrangement | Manual collection or automatic handling, bundle format and discharge direction |
| Output capacity | Accepted pieces per minute at an agreed length and hole pattern; coordinated with line cycle time |
Combined production: evaluate one C/Z line against separate machines for your product mix.
Changeover: specify frequent size changes and the manual steps operators must perform.
Output: agree finished production with punching, cutting and handling included.
Quality: confirm section, hole and length tolerances and the method used to measure them during the trial.
A CZ purlin project usually needs more detail than a simple machine name. Before requesting a quotation for a purlin machine, prepare the C and Z profile drawings, material grade, thickness range, hole pattern, cutting length, production volume,
and changeover expectation. These details help the supplier judge whether the line should prioritize quick size adjustment, punching flexibility, output speed, or a simpler operating layout.
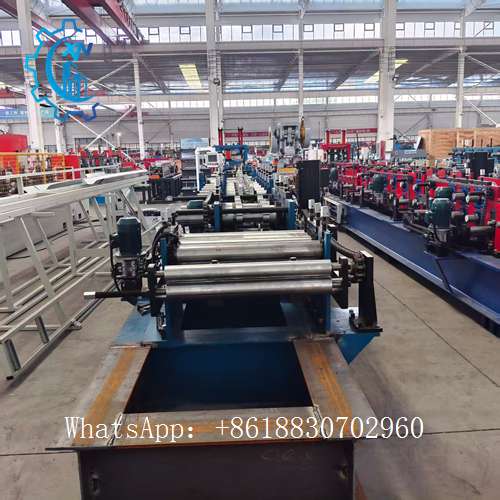
At XINNUO, we are committed to delivering high-performance metal roll forming machines tailored for global industrial needs. Our equipment offers reliable and flexible production capabilities to meet the demands of modern construction and manufacturing industries.


 8618830702960