| Delivery time: 45-60 working days. |
| Payment method: TT, 40% deposit, and the remaining balance shall be paid before delivery. |
| Warranty period: one year from the date when the machine leaves the factory. |
| Voltage: It can be customized according to the local standard industrial voltage of customers. |
| Whatsapp: +86 18830702960 |
| Work mail: xinnuo05@xinnuomachine.com |
| Website: www.xnrollformimg.com |
PTRODUCTION INTRODUCE
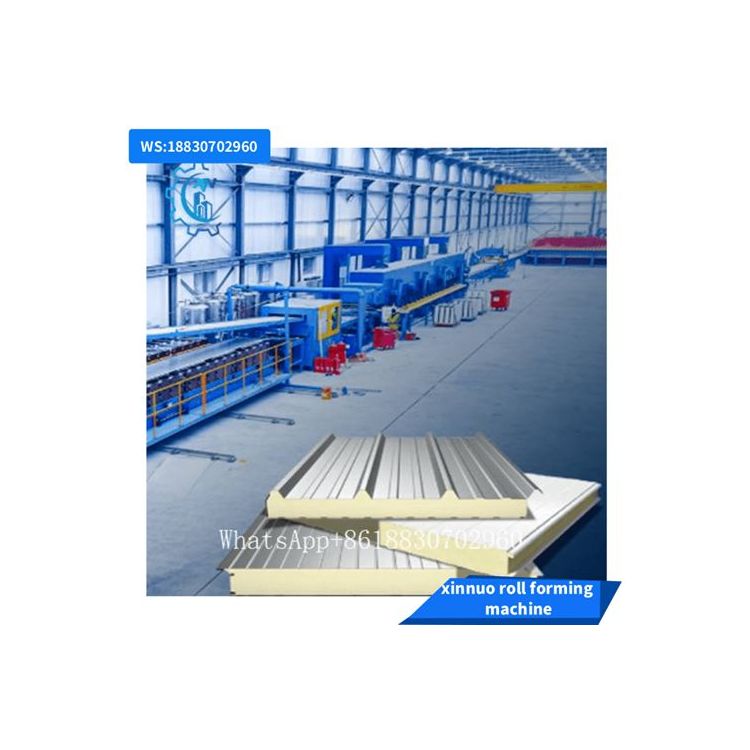
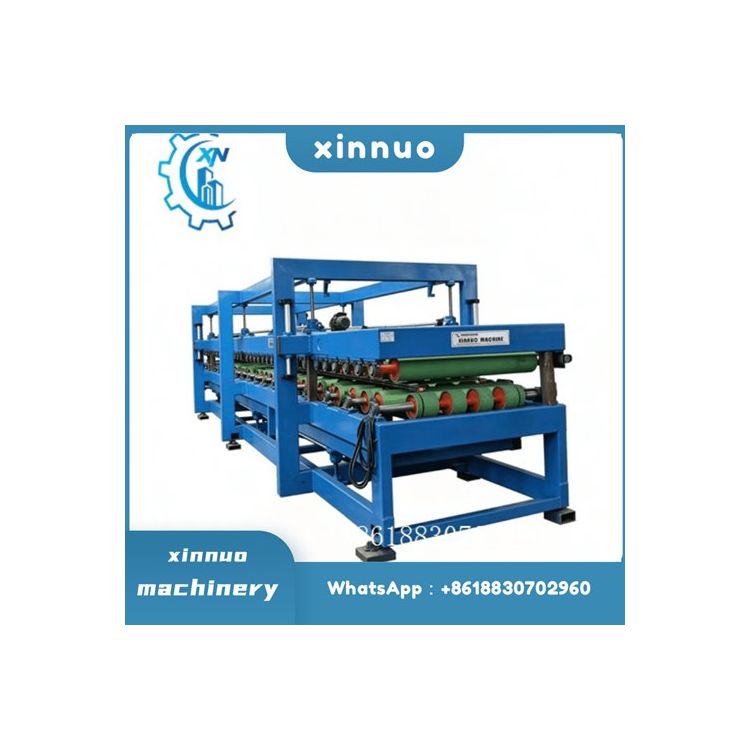
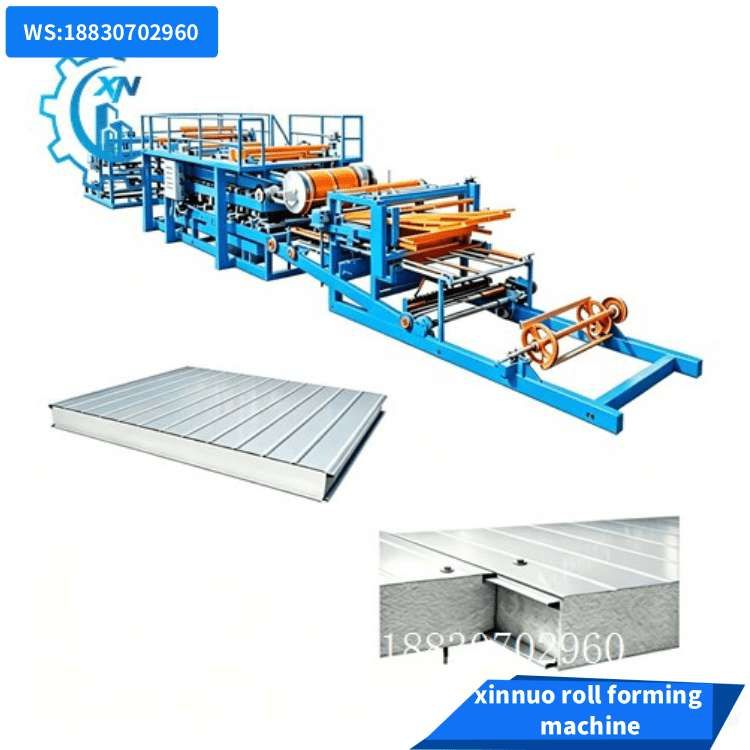
Rock wool & EPS foam composite sandwich panel adopts color steel, aluminum or stainless steel as surface sheets, with optional rock wool or EPS foam core. Rock wool version features Class A fire resistance, while EPS foam delivers excellent thermal insulation.
Available in flat and corrugated types, thickness 40–300mm, width 950–1200mm. It is lightweight, easy for fast installation, soundproof and weather-resistant, widely used for walls and roofs of prefab houses, warehouses, workshops and clean rooms.
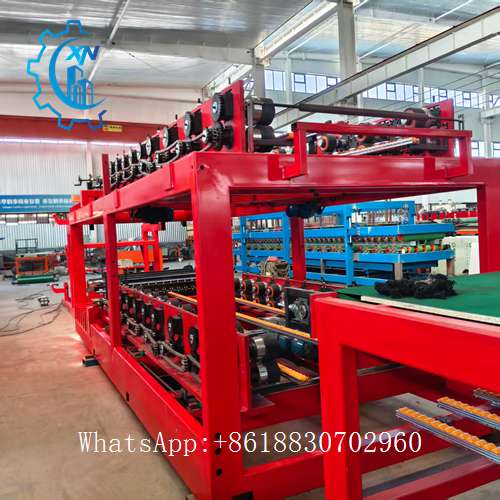
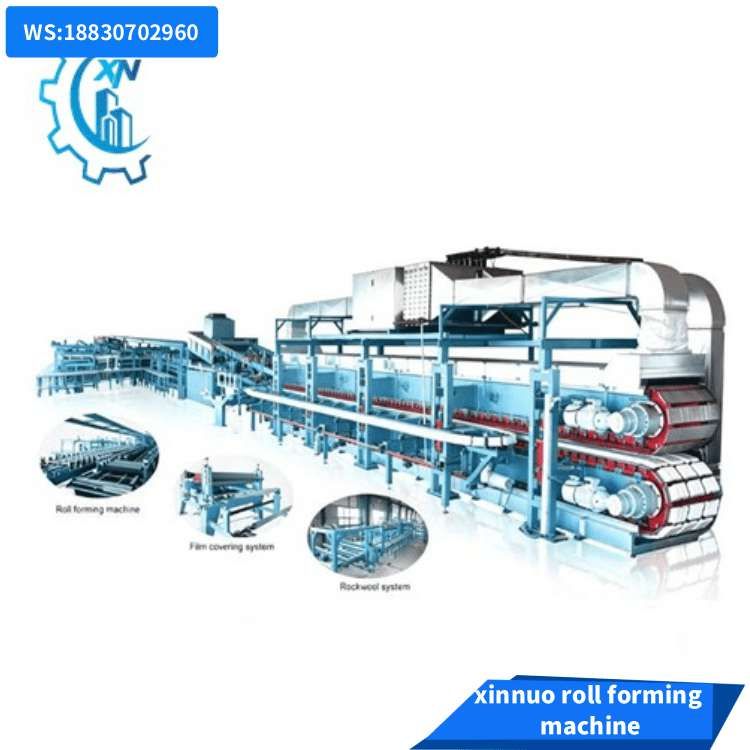
SANDWICH PANEL PRODUCTION LINE
| Item | Specification |
|---|---|
| Face Raw material | Normally 0.2-0.6 aluminum or color steel |
| Speed | 3-6m/min (Depend on the working temperature) |
| Cutting type | Trace flying saw cutting |
| Drive | Chain drive |
| Electric control system | PLC frequency conversion control |
| Core material | EPS board or rock wool |
| Total power | 35kw |
| Power supply | 380V/50HZ Or Customized |
| Annual Output | 600 thousand square meters |
| Product width | 950-1200 mm (Flat Plate) / 950-980 mm (Corrugated Composite Board) |
| Product thickness | 40-300mm |
| Equipment overall dimension (mm) | 2400021002600 / 2950021002600 |
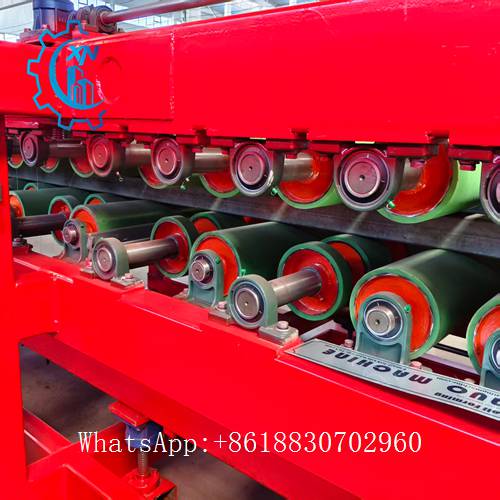
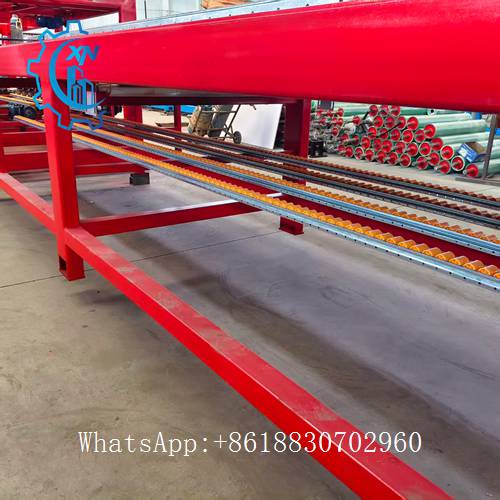
COMPONENTS OF PRODUCTION LINE
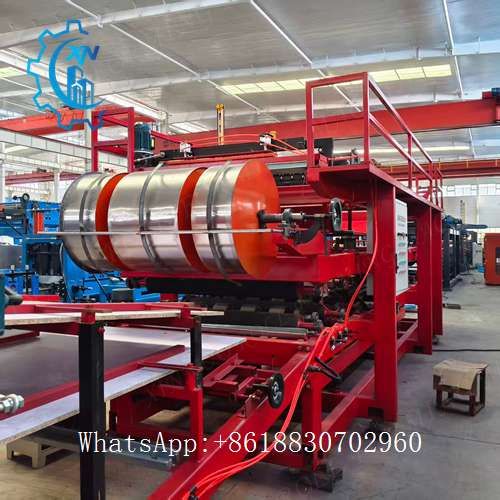
steel sheetswill be fed into the roll forming system.
2.Film coating system
This system is mainly used to protect the surface ofthe sheet.
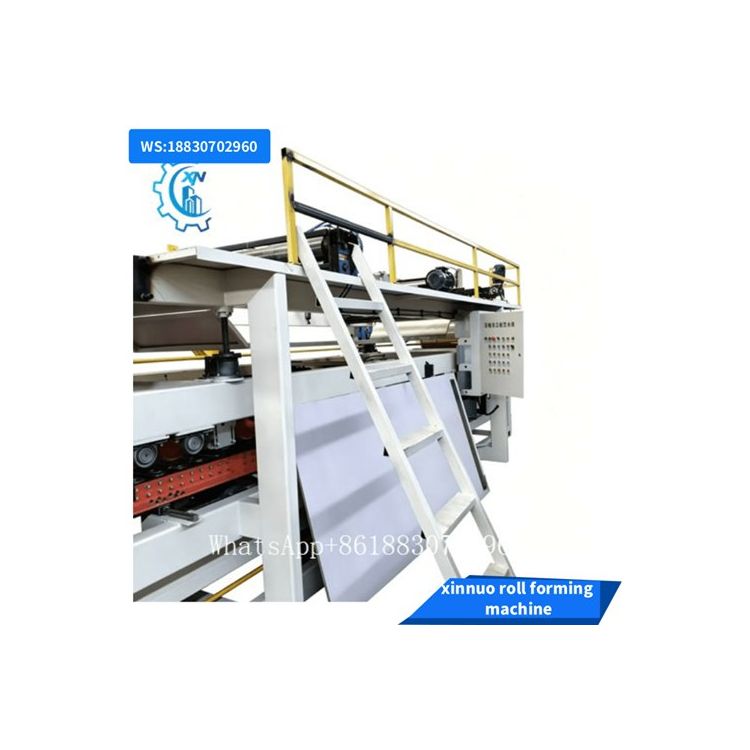
3.Roll forming system
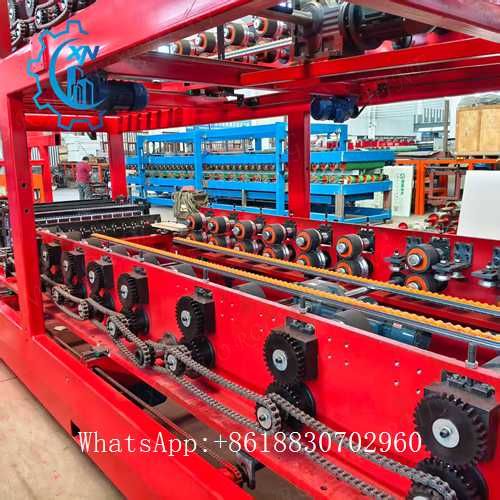
It consists of frame, transmission parts, rollers, etc.
The base frame is made of welded steel. The systemis driven by reducer and transmitted by using chain wheel and chains. The rollers are designed by CAD software and made with machining technique.
The surface of rollers is chrome plated to ensure the high hardness and long-life usage.
4.Roll forming frame
The welded structure is adopted for good rigidity. and the surface is treated by oxidation shot blasting process.
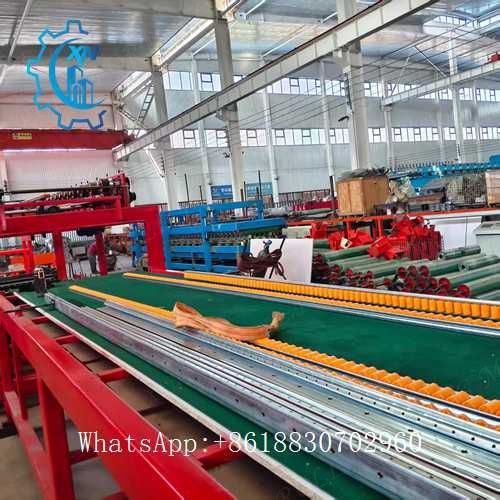
5.Insulating material feeding unit
This unit adopts framed structure. The insulating panel length should be longer than 3.5m. While the machine is running. the worker puts the insulating
panel on the feeding rollers to feed it into the laminating unit, and then it will be glued together with the upper and lower pre-painted sheets.
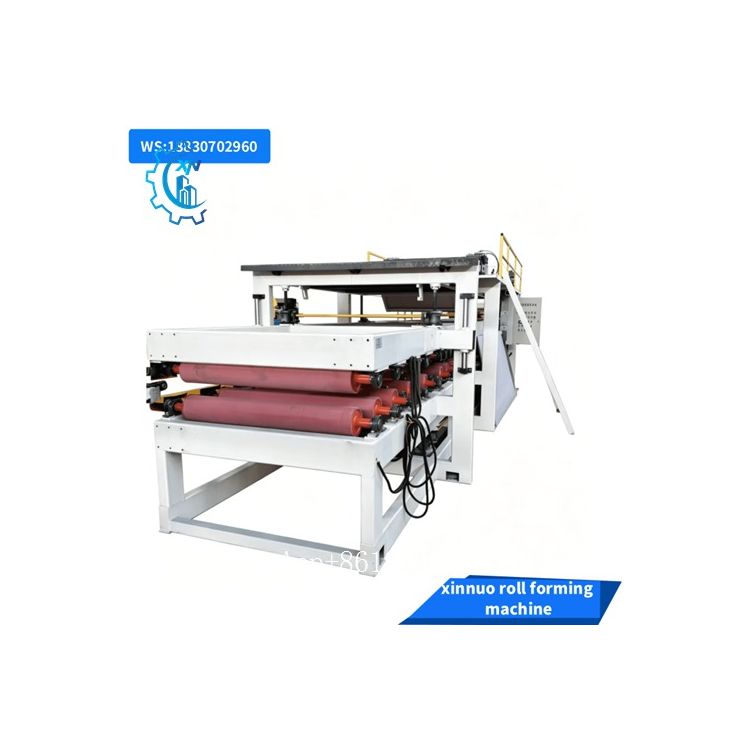
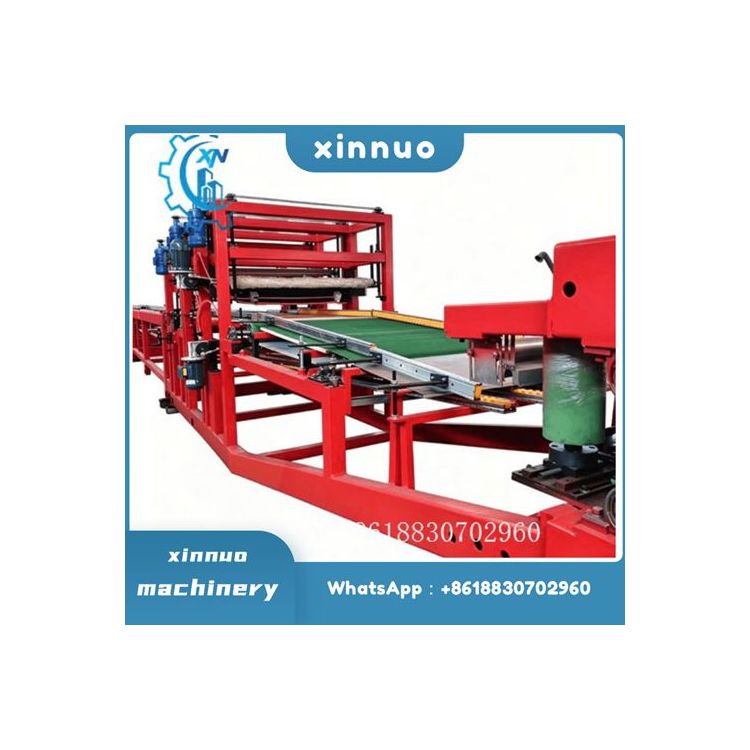
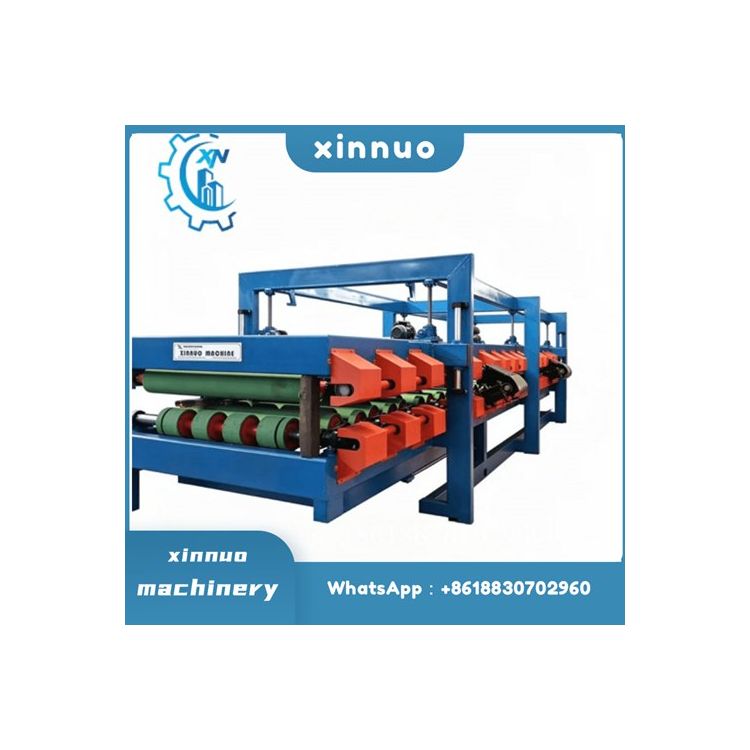
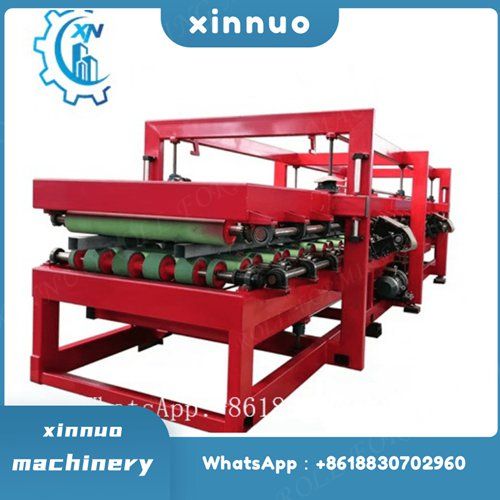
6.Laminating unit
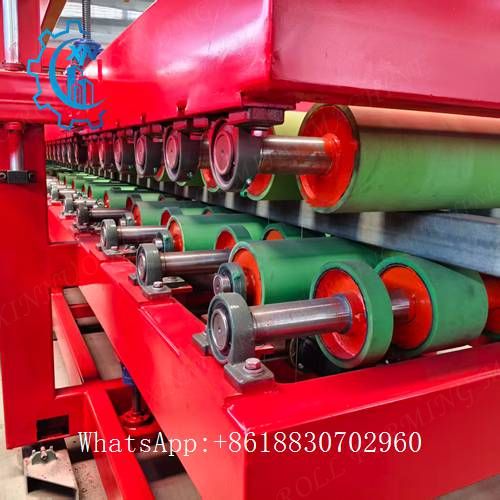
This unit is made of framed structure which has top bottom and smll total three sets of laminating roller rack Each set of roller rack s equipped
with a set of rubber coated rollers the top and bottom rubber coated rollers are applicable to flat panel and the rubber rollers on small rack is suitedor corugated panelgroove type.
The bottom rack is fixed and user can adjust the height of top rack to adjust laminating force. When producing flatDanel. the small rack s descended to the lowest postion but when
producing corugated panel. this part need to be ited to the hghest postion to be accordant with the corrugation.
7.Glue supplying system
This system is driven independenty. There are 4 drum stands to suply glue with a certain proportion to the gluing device at 4 directions The flow ofglue can be adjusted acording to the
working speed by means of glue feding motor If the ratio of two kinds of glue needs to be adusted. then should change the tooth number on the chains of the transmission shaft for each type of glue.
8.Cutting unit
This unit is equipped with a forwarding system andthe saw is driven by motor to cut off the sandwichpanel. The cutting machine features high precisioncutting. and it adopts pneumatic controlling systemfor
controlling of clamping forwarding andreserving.
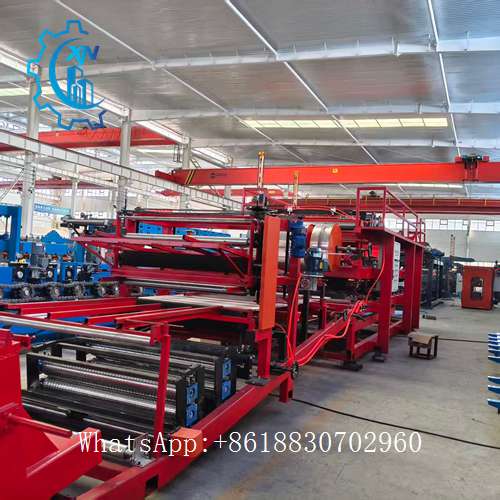
Related Products
At XINNUO, we are committed to delivering high-performance metal roll forming machines tailored for global industrial needs. Our equipment offers reliable and flexible production capabilities to meet the demands of modern construction and manufacturing industries.


 8618830702960